Contact
Why AIR?
Automated Industrial Robotics (AIR) unites technical depth, operational strength, and modern capability in a single partner built for ambitious manufacturers.
Why us
Contact
Sectors
Discover how AIR can help your drive innovation, efficiency, and scale.
Sectors overview
Medical
Driving innovation in medical device assembly, surgical instruments, orthopedic, cardiology & CRM, peripheral and continence care, and more.
Pharma
AIR partners with leading pharmaceutical companies to design, build, and support advanced automation systems for complex, highly regulated production environments.
Semiconductor
Enabling startups, global semiconductor equipment OEMs, and semiconductor fabs to scale to high-volume production systems.
Food & beverage
Proven experience across a wide range of food and beverage manufacturing processes and products including tea, bakery, pet foods, ready meals, beverage and tobacco.
Automotive
We bring the latest automation thinking, expertise, and equipment from ultrasonic welding, clipping, screwing, and snapping to materials handling, inspection, and traceability.
Consumer goods
AIR brings together deep, specialist automation expertise to deliver complex solutions across cosmetics, personal care, pet care, and electronics manufacturing.
Contact
About AIR
AIR combines deep engineering expertise, industrial scale, and advanced capability in one powerful partner for ambitious, progressive manufacturers.
Contact
Capabilities
Deep process and systems expertise, engineered to optimize performance, efficiency, and long-term operational success.
Capabilities overview
Contact
Sectors
We partner with ambitious, progressive manufacturers across the medical, pharma, semiconductor, food & beverage, automotive, and consumer goods sectors. Discover how AIR can help your drive innovation, efficiency, and scale.
Sectors overview
Contact
Sectors
Emerging technology,
semiconductor and more
AIR in Silicon Valley focuses on high-tech industries, offering specialized expertise in semiconductors, medical products, renewable energy, emerging technologies and data storage. Across our six sites, we work in a range of sectors:
See all AIR sectors
Contact
Sectors
Medical, pharmaceutical
and more
AIR in Shannon, Ireland focuses on advanced automation for the MedTech industry. Across our six sites, we work in a range of sectors:
See all AIR sectors
Contact
Sectors
Deep expertise for
progressive manufacturers
Across our six sites, we offer specialized expertise and automation innovation to a range of sectors:
See all AIR sectors
Contact
Sectors
Pharma, medical, food and beverage,
consumer goods and more
Across our six sites, AIR works in a range of sectors:
See all AIR sectors
Contact
Sectors
Medical devices, filling
machines and more
AIR in Sligo, Ireland delivers advanced automation solutions for medical and life sciences manufacturers, including flexible filling systems and high-speed filling systems. Across our six sites, we work in a range of sectors:
See all AIR sectors
Contact
Sectors
Deep automotive
expertise and more
AIR in Rochester Hills specializes in the design and manufacture of fully integrated stand-alone assembly, specialized machines, and automated and secondary assembly equipment. Across our six sites, we work in a range of sectors:
See all AIR sectors

Just-in-time clinical trials manufacturing system accelerates drug introduction

Project snapshot
Client:
Medicines Manufacturing Innovation Centre (MMIC)
Location:
Scotland, UK
Sector:
Product type:
Automated clinical trials manufacturing system
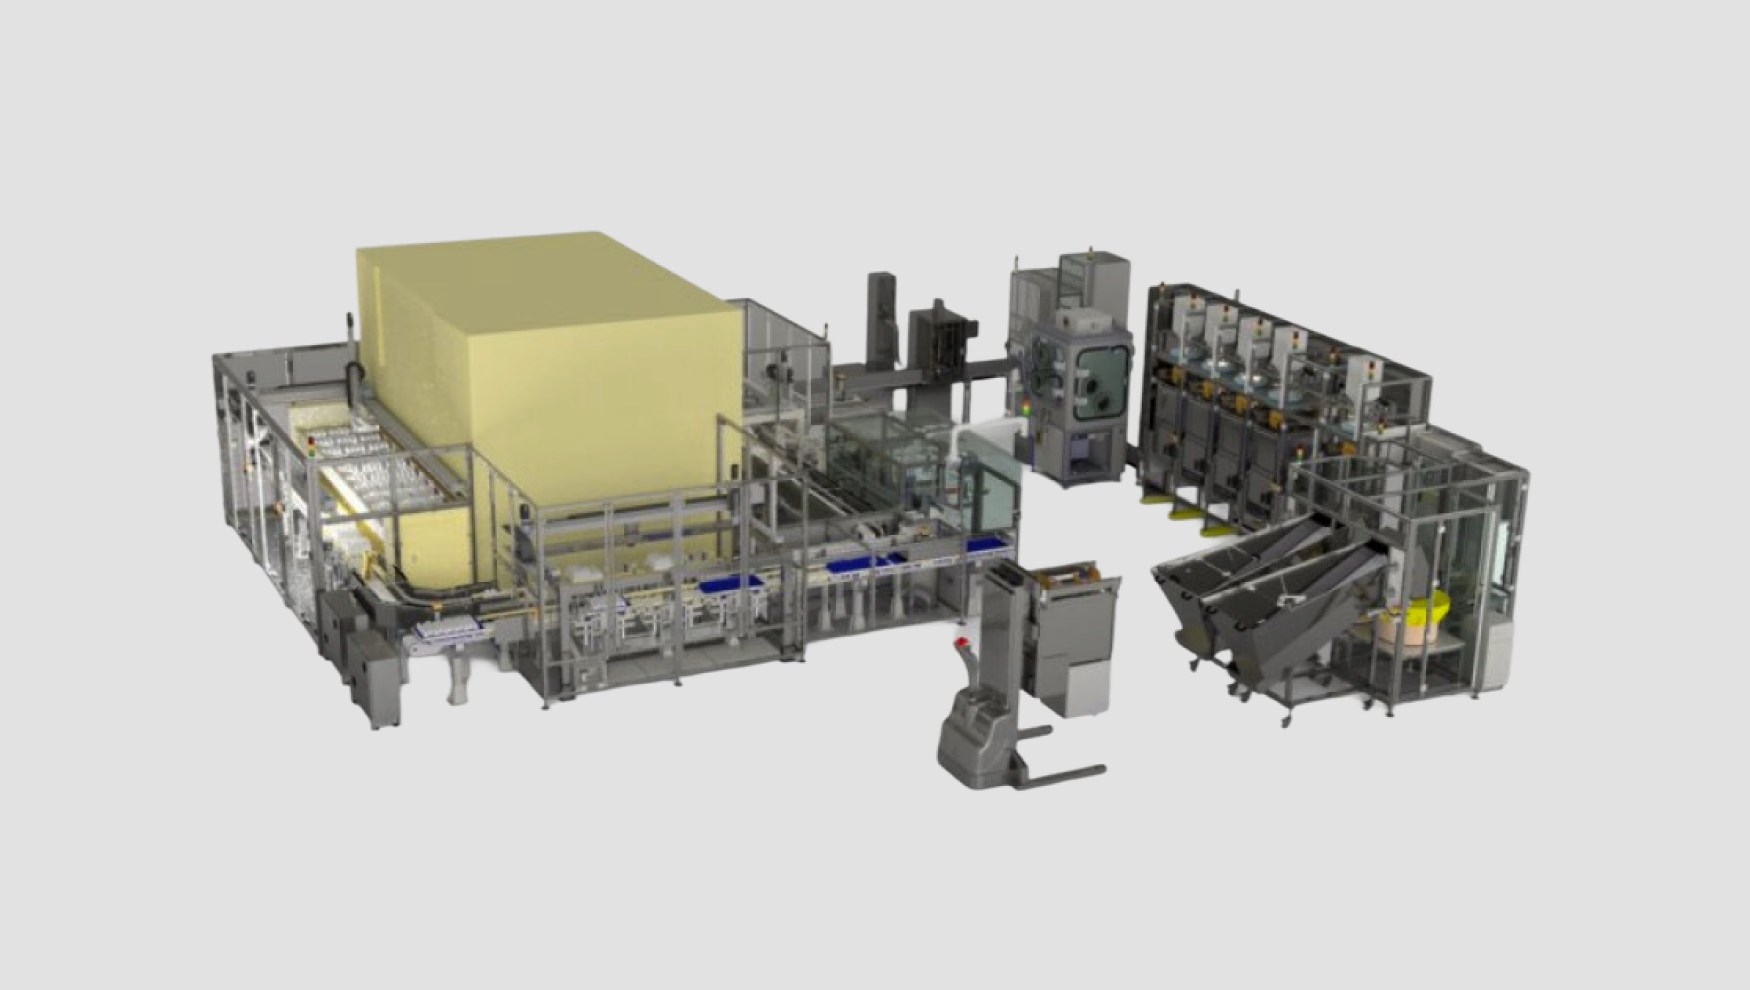
Rendering of a just-in-time clinical trials manufacturing line
Challenge

Minimizing time to introduce new medicines

Scotland’s Medicines Manufacturing Innovation Centre (MMIC) required a manufacturing system capable of rapidly introducing new medicines into clinical trials while maintaining pharmaceutical hygiene standards, eliminating cross-contamination risk, and ensuring full product traceability. The system needed to support tablets and capsules, multiple bottle sizes, frequent changeovers between drug types, and strict environmental control—without placing the entire line in an ISO-class clean room.

Innovation

A modular, fully automated, traceable manufacturing platform

AIR delivered a turnkey clinical trials manufacturing system composed of integrated modules that support flexible, small-batch pharmaceutical production while maintaining strict cleanliness and traceability.

Key innovations included:

  • Modular system architecture supporting handling, filling, sealing, weighing, marking, labeling, storage, and packing
  • Individual filling modules with humidity and temperature monitoring, eliminating the need for a full clean room environment
  • Laser marking of each bottle with a unique 2D matrix code for end-to-end traceability
  • Independent drug filling modules designed for rapid changeover between drug types and strengths
  • Integrated weighing and verification steps linked to bottle ID to confirm correct desiccant and drug loading
  • Extensive automated bottle and tray storage, retrieval, and routing capability supporting over 17,000 bottles
  • Dedicated labeling system with machine-vision verification prior to label application
  • Unique digital dashboard allowing for drugs to be signed off remotely, eliminating hours of paperwork
Result

Flexible, scalable clinical trials manufacturing with full traceability

The completed multi-million-pound system enables MMIC to rapidly manufacture clinical trial medications with full bottle-level traceability, reduced contamination risk, high operational flexibility, while reducing stock inventory requirements and overall cost of clinical trials. By localizing environmental control within individual process modules, the system meets pharmaceutical hygiene requirements while avoiding the complexity of a full clean-room installation. The scalable architecture supports future capacity growth and new packaging formats, helping accelerate the path from development to clinical trials.

Case studies

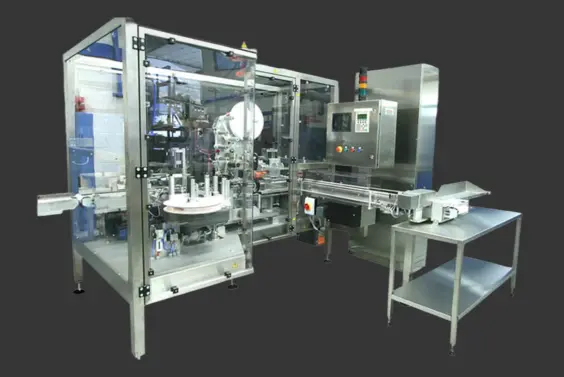
A leading pharmaceutical company needed an automated solution capable of applying tamper-evident labels and unique device identification (UDI) labels to a variety of pharmaceutical cartons at high speed.
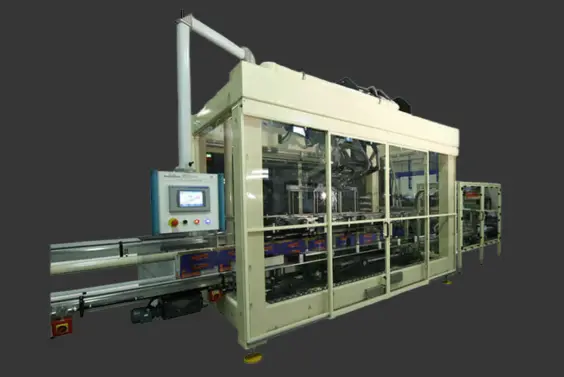
A producer in the bakery industry producing biscuits for retail required a robust automated packaging solution capable of handling demanding, high-volume production requirements. The system needed to deliver…
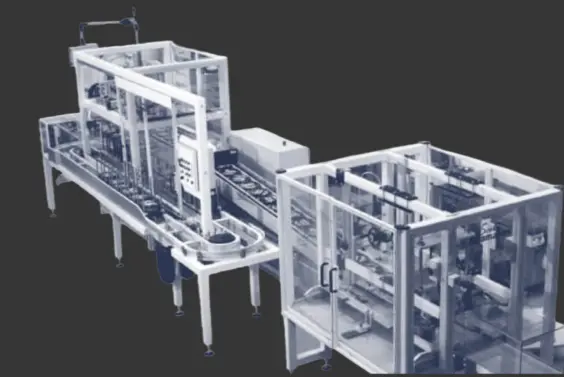
One of the world’s largest confectionery manufacturers wanted to automate the process of lidding tubs of individually wrapped chocolates. The system needed to pick and place multiple lid types made from…

View all case studies
Contact us

Let’s talk

Talk to AIR’s team about your latest manufacturing challenge. We’re here to help you bring your latest innovations to market quickly and at scale. Ideating, designing, building, commissioning, and supporting your next wave of automated manufacturing.