Automated palletization systems designed to accelerate your production line
We offer a range of palletizing systems — from collaborative robot cells through to full industrial palletizing cells with integrated labeling — each designed to fit the specific requirements of your facility. Our systems are pre-tested before delivery, fast to install, and built to operate reliably across long production runs with minimal disruption to your operation.
Capabilities
Palletizing systems to suit your production environment, space, and volume requirements
We offer three proven palletizing system configurations, each developed in-house and configurable to your factory layout, product type, and throughput needs. All systems support multiple conveyor types, flexible pallet patterns, and touch-screen HMI control for straightforward day-to-day operation:
Cobotic (collaborative robot) palletizer
A cobot palletizing cell designed for dynamic palletization of cases and boxes. Because collaborative robots don’t need safety fencing or light curtains, this solution has a smaller footprint and lower overall cost than traditional industrial robot cells. The system handles payloads from 0.5kg to 14kg, reaches speeds of up to 20 cases per minute with multiple case picks, and can be configured with one or two product in-feeds. Starting from 2m x 2m, it’s well suited to facilities where floor space is limited.
Options
- Adaptions to any factory setting with RDS designs
- Improvements and upgrades to allow for a second pallet zone and more
Standard palletizing cell
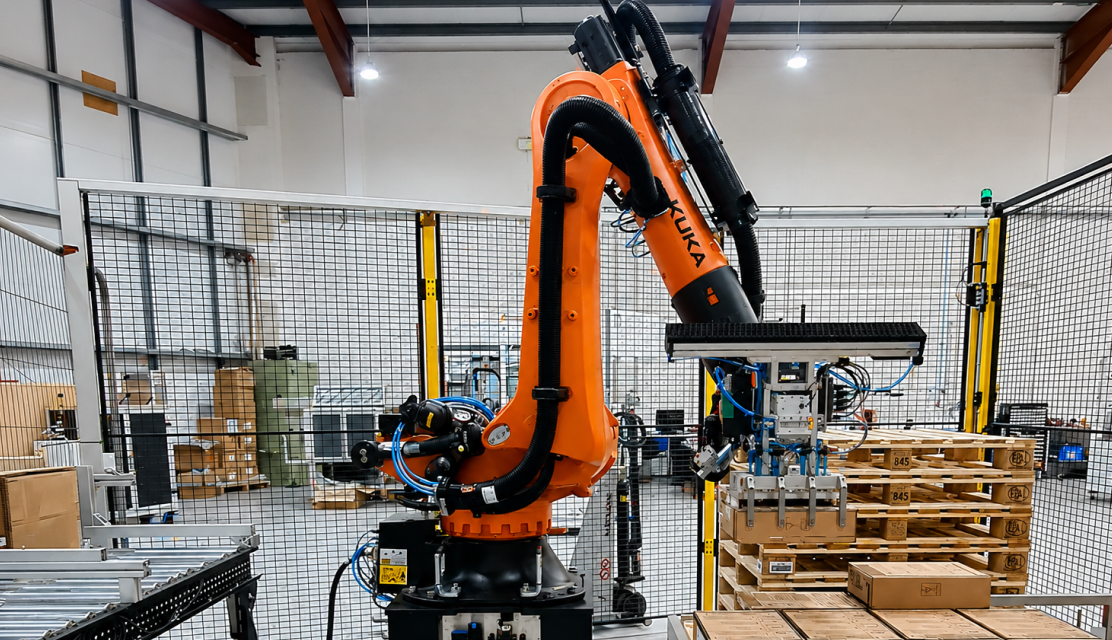
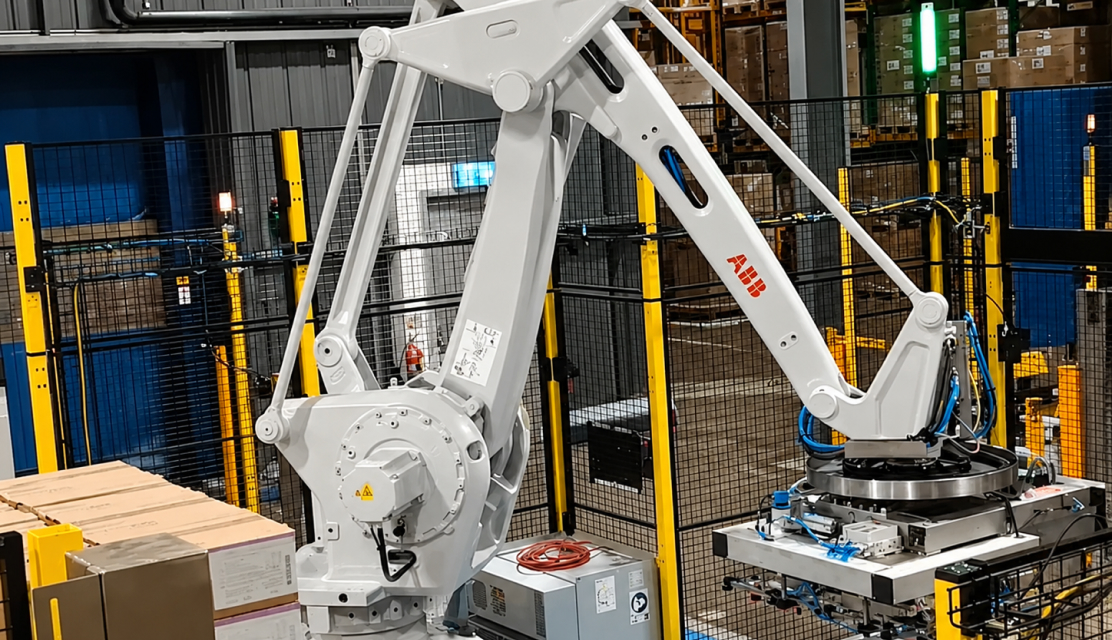
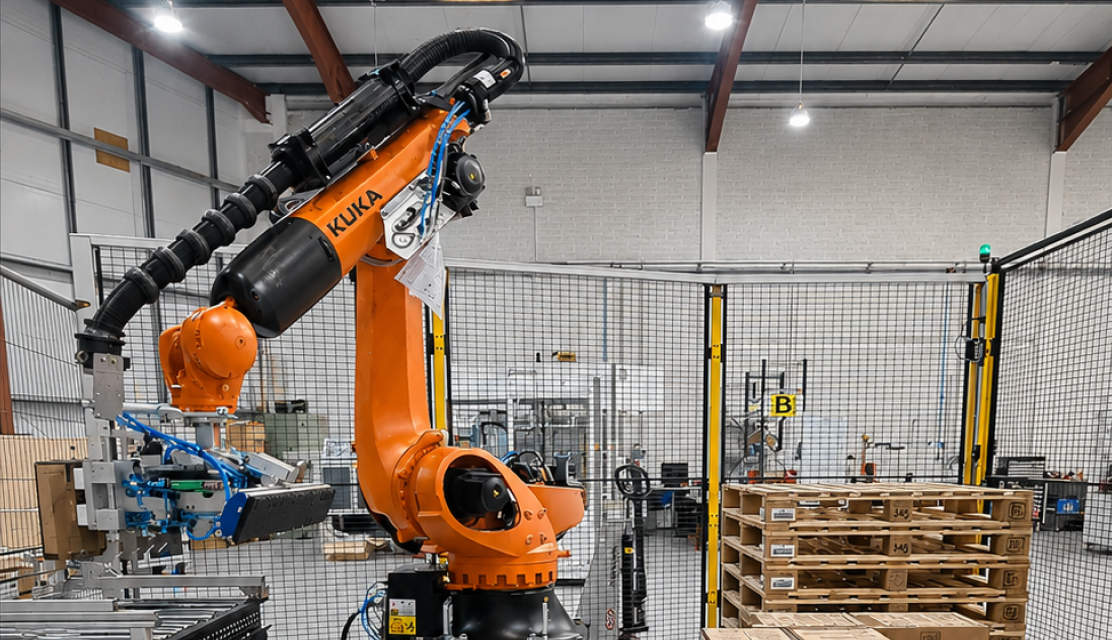
An industrial robot palletizing cell using the latest conveyor technology and multi-position pick programming to palletize boxes efficiently at up to 20 cases per minute, with a maximum payload of 250kg. The cell uses a 90-degree box reorientation system on the conveyor to bring products precisely to the robot pick position, with accumulation processes allowing the robot to pick multiple boxes simultaneously for greater throughput. A full CE-certified safety system is integrated as standard.
Options
- Choice of two pallet zones to reduce downtime
- Robot options available depending on the requirements
- Multiple pick positions available
- Multiple product in-feed available with configurable conveyor accessories
Label application and palletizing cell
A compact, dual-function cell that automates both labeling and palletization in a single integrated system. Boxes are labeled by inline applicators as they travel along the conveyor, then picked and palletized by the robot across two pallet zones. A sliding door with sensor interlocks allows one full pallet to be unloaded while the robot continues to work in the second zone, delivering continuous operation with near-zero changeover downtime.
Options
- Choice of two pallet zones to reduce downtime
- Robot options available depending on the requirements
- Multiple pick positions available
- Multiple product in-feeds available with configurable conveyor accessories
Across all three systems:
- Configurable pallet patterns, sizes, and layer configurations via touchscreen HMI
- Multiple gripper options including vacuum, clamp, and grappler types
- Compatible with belt, roller, and gravity conveyor types
- Allen Bradley, Siemens, or Omron control systems available
- CE-certified safety systems included as standard across all configurations
- Remote diagnostics capability, allowing engineers to log in and resolve issues without an on-site visit
- Performance monitoring with statistical feedback including picks per hour, pallets completed per day, and fault reporting
- Pre-tested prior to delivery for fast installation and minimal production disruption
Approach
Configured to your requirements, delivered and supported by our own engineers
We design each system around the specifics of your production environment — your floor space, your product, your throughput targets, and your existing line layout. All systems are built and tested in-house before delivery, and our engineers manage installation and commissioning on-site.
- Open, agile, early-stage explorations
- Detailed examinations of downstream and upstream processes
- Detailed examinations of the product, containers, and manufacturing requirements
- Assembly of the best-fit, cross-functional AIR team for the project
- Delivery of an initial proof-of-concept project when required
- Building and maintaining close, open, collaborative relationships throughout
- Factory acceptance testing, installation, commissioning, and lifecycle support
Impact
Reliable end-of-line automation that reduces cost, improves throughput and frees your workforce
Automating palletization with AIR delivers clear, measurable benefits to production efficiency, operating costs, and the working environment for your team.
- Consistent palletization speeds of up to 20 cases per minute, maintained reliably across full production shifts
- Significant reduction in manual handling at end-of-line, reducing physical strain and associated injury risk for operators
- Near-zero downtime during pallet changeovers through dual pallet zone configurations, keeping the robot working continuously
- Reduced overall cell cost and floor space requirements with collaborative robot options that eliminate the need for safety fencing and light curtains
- Flexible operation across multiple product formats, pallet patterns, and case sizes without lengthy reprogramming
- Combined labeling and palletization in a single integrated cell, removing a separate manual process from the line entirely
- Full production visibility through statistical monitoring, giving supervisors accurate data on throughput, faults, and performance
- Fast return to operation following any issue through remote diagnostics and rapid on-site support from our engineering team
Case studies
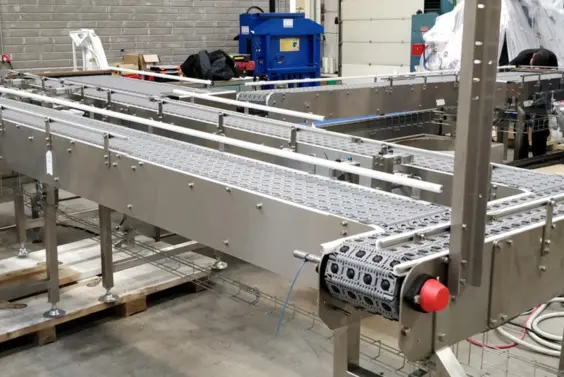
The aim of this project was to implement new technologies to improve the efficiency and simplify the palletizing process of boxed product. One challenge was to achieve the end goal but still minimize the…
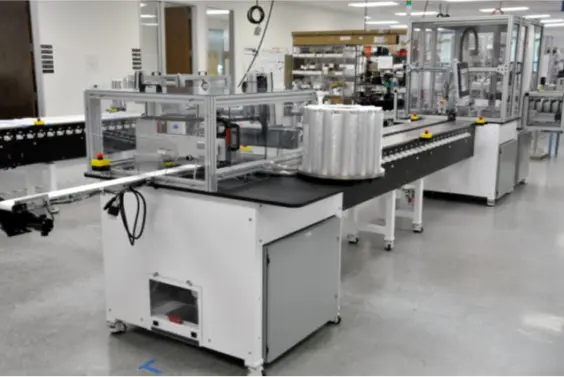
A medical device diagnostic manufacturer needed to rapidly replicate an in-house designed manufacturing tool to support a production ramp-up. The tool included multiple control systems and needed to be…
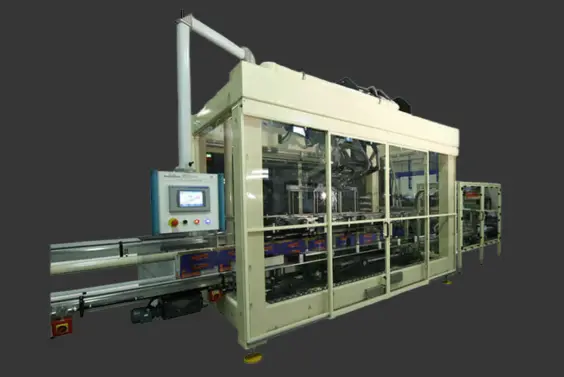
A producer in the bakery industry producing biscuits for retail required a robust automated packaging solution capable of handling demanding, high-volume production requirements. The system needed to deliver…