High-speed pharmaceutical labeling and serialization for secure product traceability
Project snapshot
Client:
Location:
Sector:
Product type:
Challenge
Applying tamper and UDI labels at production speed
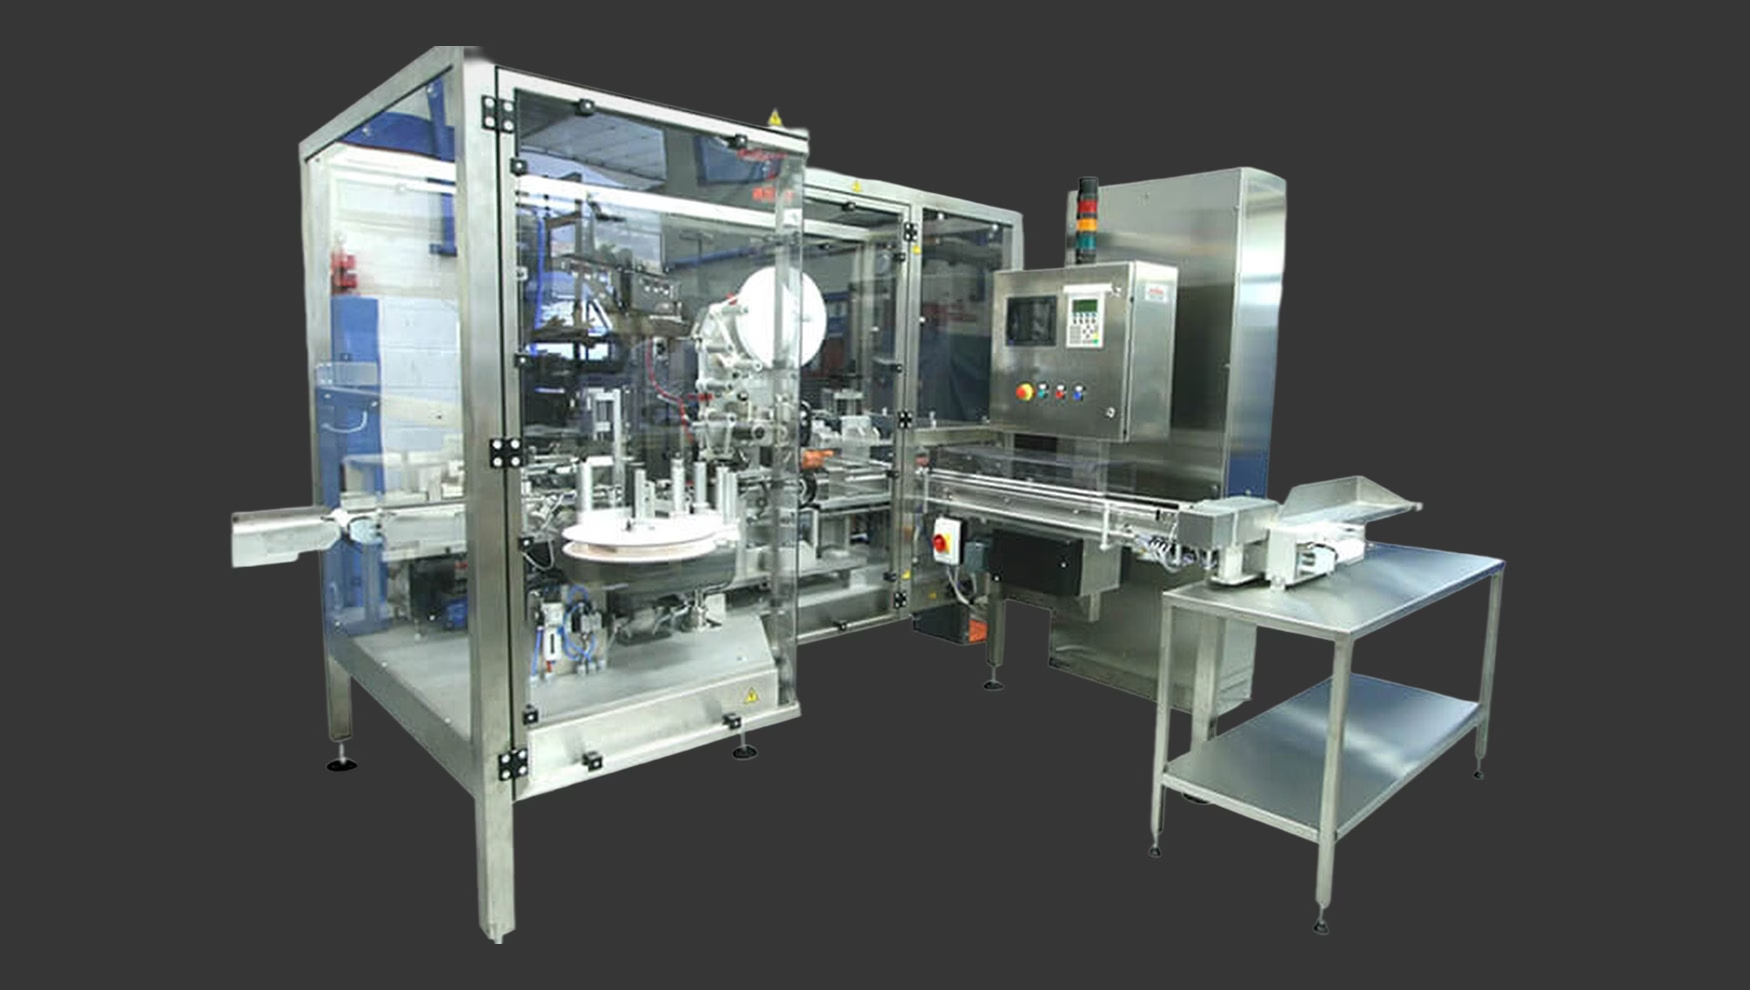
A leading pharmaceutical company needed an automated solution capable of applying tamper-evident labels and unique device identification (UDI) labels to a variety of pharmaceutical cartons at high speed.
The system also had to integrate seamlessly with an existing checkweigher, requiring controlled product transfer into and out of the labeling process while maintaining traceability and quality standards. The solution needed to support multiple carton sizes and feed reliably into the next stage of the packaging line.
Innovation
Fully automated, vision-verified labeling and serialization
AIR designed a bespoke pharmaceutical labeling and serialization system to ensure accurate label placement, verification, and data capture at speed, while maintaining flexibility for different carton formats.
- Fully automated labeling system for high-volume pharmaceutical cartons
- Adjustable flighted conveyor to orientate cartons by 90° and accommodate multiple sizes
- Application of two tamper-evident labels across opening flaps and cross-locks on larger cartons
- Custom vision system to verify product orientation prior to labeling
- Post-application vision inspection to confirm label presence, position, and code accuracy
- Serialization data verification with feedback to a central database for full supply chain traceability
- Integrated reject handling for non-conforming products
Result
Flexible, validated labeling with full traceability
The system operates at 50 units per minute and supports multiple carton sizes with tool-free changeover via hand dials. Designed for ISO8 cleanroom operation, the solution was delivered with a full validation documentation package, including FSDS, FMEA, operator and maintenance manuals, and IQ documentation completed on borders.
The result is a robust, high-speed labeling and serialization platform that enables secure traceability throughout the pharmaceutical supply chain.
Featured capabilities:
Featured sectors:
Case studies
Scotland’s Medicines Manufacturing Innovation Centre (MMIC) required a manufacturing system capable of rapidly introducing new medicines into clinical trials while maintaining pharmaceutical hygiene…
A producer in the bakery industry producing biscuits for retail required a robust automated packaging solution capable of handling demanding, high-volume production requirements. The system needed to deliver…
One of the world’s largest confectionery manufacturers wanted to automate the process of lidding tubs of individually wrapped chocolates. The system needed to pick and place multiple lid types made from…