High-performance custom automated conveyor systems for integrated production environments
Automated and industrial conveyor systems play a vital role in modern manufacturing, facilitating the controlled movement, positioning, and accumulation of products along production lines. From high-speed assembly to intricate material handling settings, selecting the right conveyor system is essential for maximizing throughput, efficiency, and reliability. AIR designs and manufactures conveyor systems for leading companies across various industries, providing solutions customized to specific products, processes, and production needs.
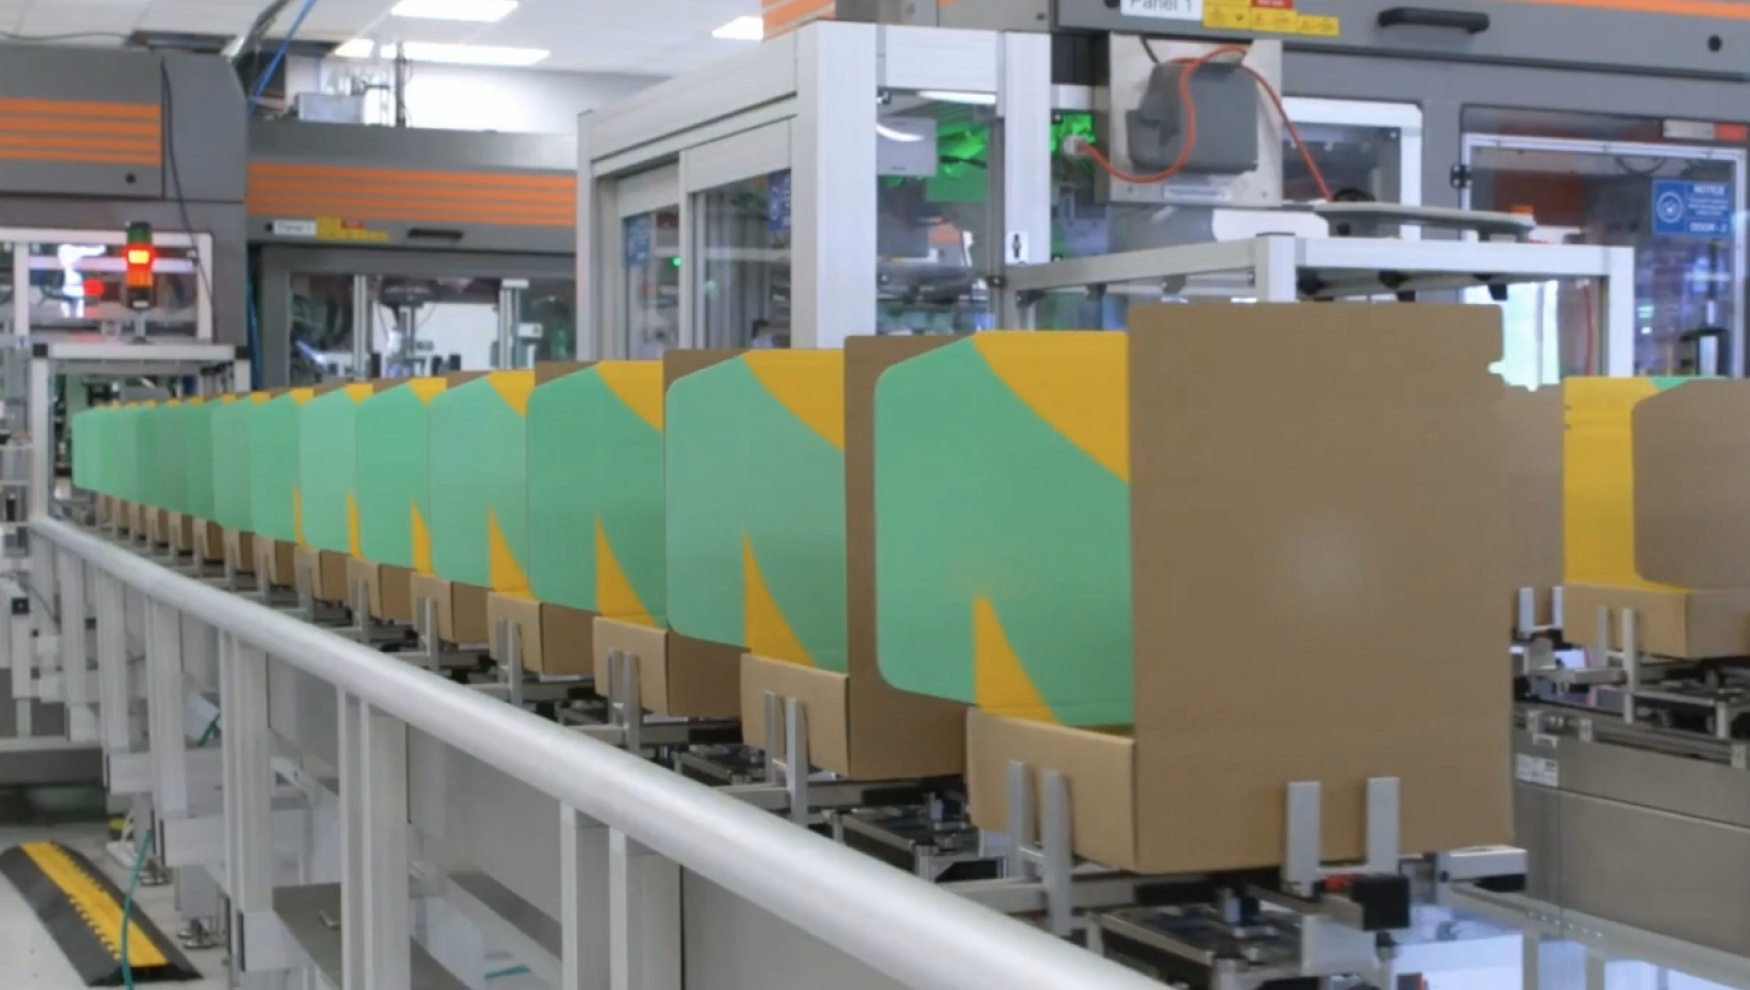
Capabilities
Flexible, high-performance conveyor systems, engineered for precision and flow
As a conveyor systems manufacturer and integrator, AIR delivers automated conveyor systems and industrial conveyor systems designed to support efficient product flow, accurate positioning, and seamless integration with upstream and downstream equipment. Our material handling conveyor systems are engineered for performance, flexibility, and long-term reliability across demanding production environments.
- Precision link conveyorsDesigned for high-speed, high-accuracy applications, offering precise positioning, high load capacity, and smooth movement, available in both servo- and cam-driven configurations.
- Indexing rotary assembly turrets and ring turretsEnable efficient, repeatable assembly by rotating and indexing products to defined positions for specific operations.
- Intelligent racetrack systemsIntegrated motion platforms using specialist software to create flexible, high-speed production flows, increasing output and reducing downtime.
- Custom servo-controlled racetracksConfigured across single- or multi-axis systems (1–4 axis), providing full control over speed, positioning, and system behavior.
- Flighted conveyor systemsAllow controlled movement and elevation of components to support efficient product handling during assembly processes.
- Belt and modular chain conveyor systemsRobust and reliable solutions widely used in industrial conveyor systems and material handling conveyor systems, particularly where precise positioning or orientation is not required.
- Puck-based conveyor systemsUsed within automated conveyor systems for handling small or fragile products, carrying items securely through the production line on individual pucks.
- Pallet-based conveyor systemsEnable single-piece flow, adaptable to different sectors, product types, and production environments.
- Walking beam systemsHigh-performance transfer systems using servo technology to deliver fast, accurate movement where traditional conveyors aren’t suitable.
Approach
Engineering conveyor systems as part of complete production solutions
AIR approaches conveyor system design as part of the wider production process — not as standalone equipment. This ensures that material flow, system integration, and operational performance are fully aligned.
- Early-stage evaluation of product flow, throughput, and process requirements
- Detailed analysis of upstream and downstream integration points
- Selection of the most appropriate conveyor technologies based on product characteristics and handling needs
- Design of systems to manage accumulation, buffering, orientation, and transfer
- Integration with robotics, inspection, filling, assembly, and packaging systems
- Development of modular architectures to support flexibility, expansion, and future reconfiguration
- Implementation of control systems to synchronize motion, optimize flow, and reduce downtime
- Focus on reliability, maintainability, and long-term operational performance
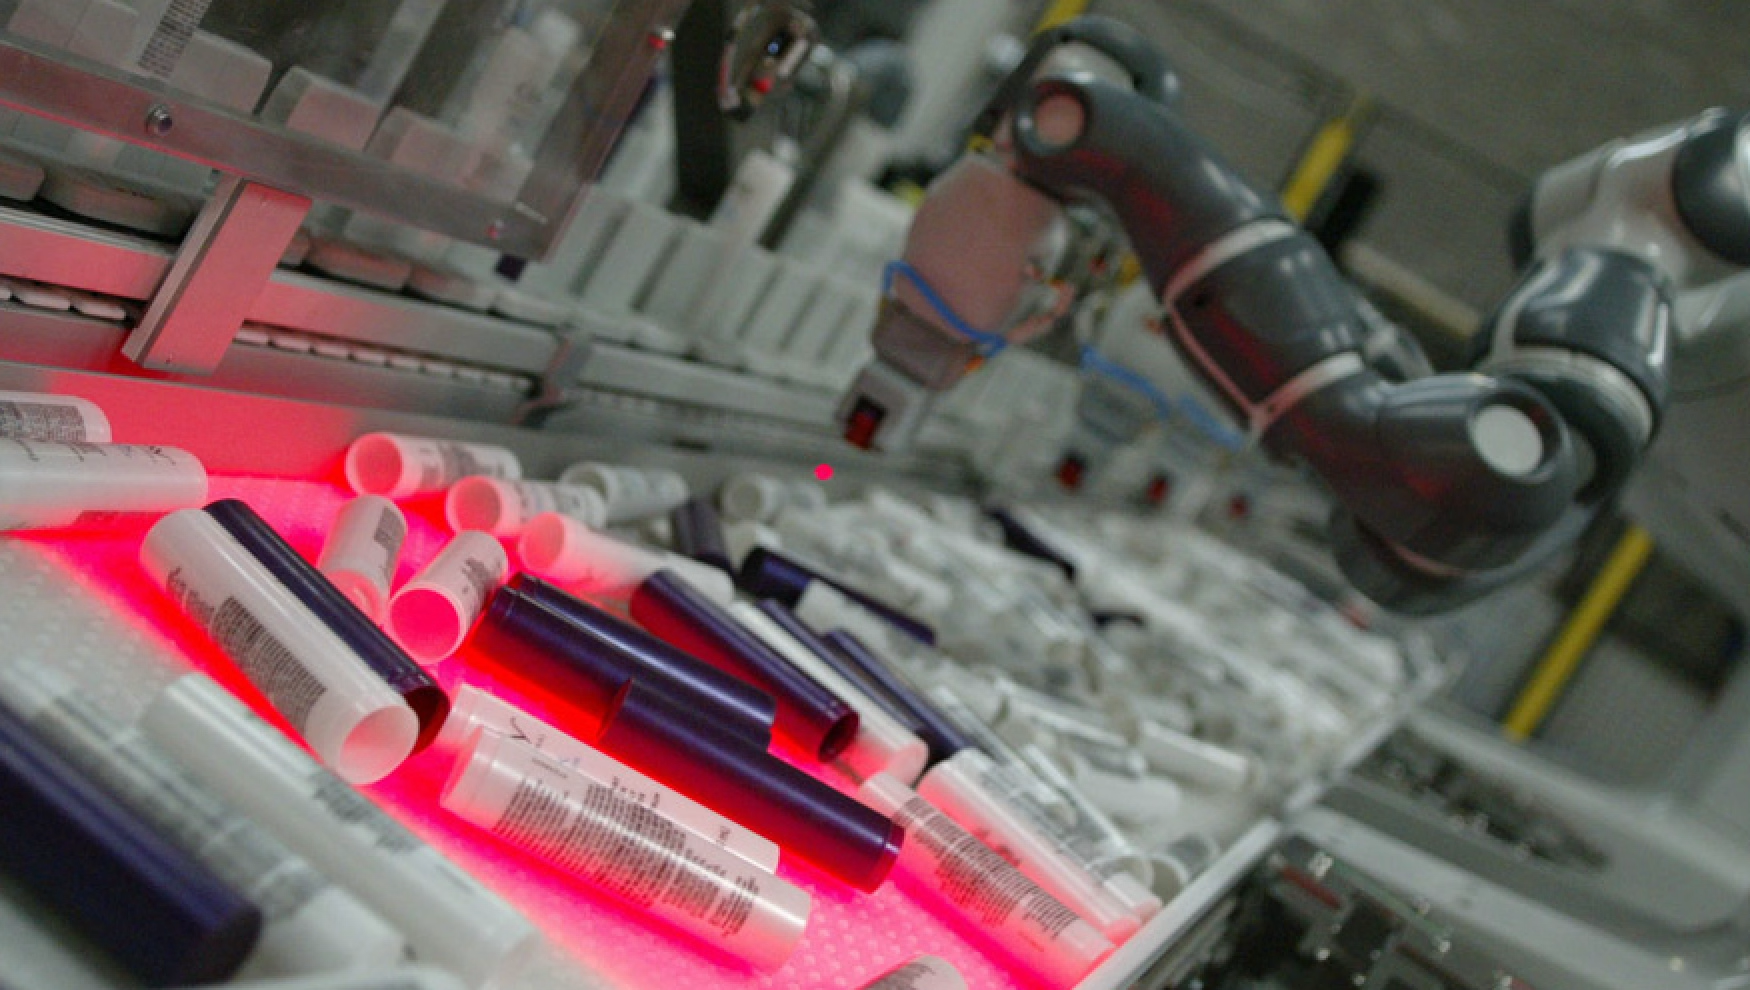
Impact
Delivering efficient flow, reliability, and scalable performance
Well-designed conveyor systems are fundamental to efficient, high-performing production lines. By ensuring smooth, controlled product movement, they enable greater consistency, higher throughput, and reduced operational risk. AIR’s conveyor systems are designed to deliver measurable outcomes, including:
- Optimized product flow and reduced bottlenecks
- Increased throughput and improved line efficiency
- Accurate and repeatable product handling
- Reduced manual handling and associated risk
- Flexibility to support multiple products and changeovers
- Reliable operation in demanding production environments
- Scalable systems that support future expansion and process changes
Case studies
A major HDD manufacturer needed to improve the reliability and cleanliness of their media scrubber modules without replacing the entire cleanline. Existing automation dropped disks frequently, had low…
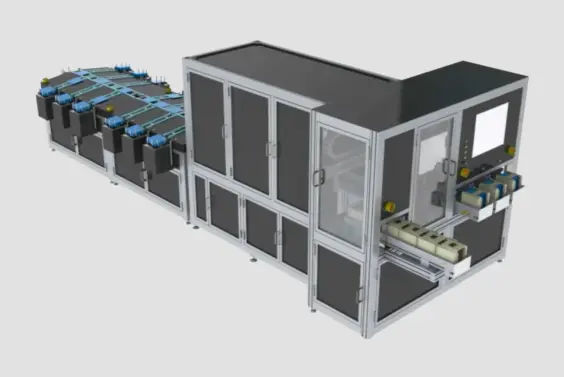
A leading solar panel manufacturer needed to integrate proprietary, cost-reducing processes into production using custom equipment. Internal teams faced competing priorities, and any delay risked missing…
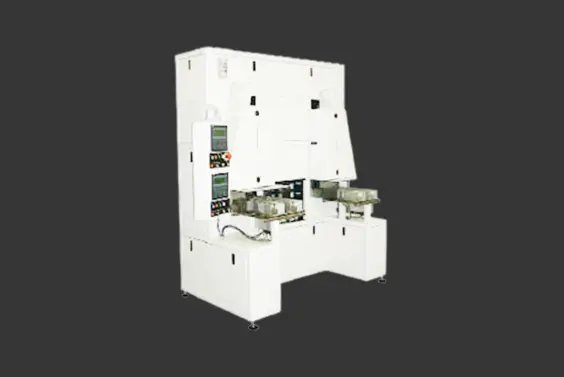
A major hard disk manufacturer had developed a lab-scale UV processing technology and needed to scale it to high-volume production. The system had to handle media at high speed, integrate seamlessly with…