Designers and integrators of product serialization and track-and-trace systems
AIR designs and integrates product serialization and track-and-trace systems that give manufacturers complete visibility over every unit, batch, or component across the production process. Working with companies in pharmaceutical, medical device, food, cosmetics, tobacco, and industrial manufacturing, we build systems that assign, capture, and store unique product identities — enabling full traceability, faster recalls, and regulatory compliance from line to end customer.
Capabilities
Custom, end-to-end serialization and traceability systems
AIR delivers track and trace systems designed to capture and record product data at every stage of manufacturing and packaging — from individual unit serialization through to batch aggregation and supply chain handoff. Our systems are built around your process, your compliance requirements, and your existing line infrastructure.
- Product serializationAssigning unique identifiers — barcodes, QR codes, Data Matrix codes, or RFID tags – to individual products or packaging units, creating a permanent, scannable record tied to production data.
- Batch and lot traceabilityLinking individual serialized units to batch or lot records, enabling fast isolation and investigation of any quality or compliance issue without disrupting the wider line.
- Aggregation and hierarchy trackingBuilding parent-child relationships between units, cartons, cases, and pallets — so every level of your packaging hierarchy is accounted for and traceable.
- Vision and verification systemsIntegrating camera-based inspection and code verification to confirm that every label is applied correctly, every code is readable, and no unit leaves the line without a valid identity.
- RFID and barcode technologiesSupporting a broad range of identification technologies, selected based on product type, read distance, environment, and throughput requirements.
- Data capture, storage, and reportingConnecting serialization hardware to your MES, ERP, or standalone traceability database — ensuring data is structured, accessible, and audit-ready.
Impact
Traceability that protects your product, your customers, and your business
Serialization and track and trace systems are increasingly a regulatory requirement in pharmaceutical and food manufacturing — but the operational value goes well beyond compliance. AIR ensures every product has a verifiable identity and history, so you can respond faster to quality issues, reduce the cost of recalls, and give customers and regulators the confidence they need.
- Rapid identification and isolation of defective units or batches, reducing the scope and cost of recalls
- Full audit trail from component or raw material through to finished product and dispatch
- Regulatory compliance for pharmaceutical serialization mandates (DSCSA, EU FMD, and others)
- Reduced risk of counterfeiting, diversion, or gray-market activity
- Faster resolution of customer complaints and field investigations
- Improved batch release processes and quality reporting
- Data foundation for broader process analytics and continuous improvement
Approach
Building traceability into your line, not bolted on after
Track and trace systems work best when they’re part of the production architecture from the beginning — integrated with conveyors, packaging equipment, inspection systems, and data infrastructure rather than added at the end. AIR designs traceability solutions as part of the wider line, not as standalone hardware.
- Early-stage review of product type, packaging format, regulatory requirements, and existing data infrastructure
- Selection of the most appropriate identification technology (barcode, Data Matrix, QR, RFID) based on the application
- Design of label application, code generation, and verification processes suited to line speed and format
- Integration with upstream and downstream equipment including filling, packaging, and end-of-line systems
- Connection to MES, ERP, or purpose-built traceability platforms for data capture and reporting
- Validation support for regulated environments, including IQ/OQ/PQ documentation where required
- Modular architecture enabling future expansion: additional lines, new products, evolving regulatory requirements
- Ongoing support and system updates as standards or production requirements change
Case studies
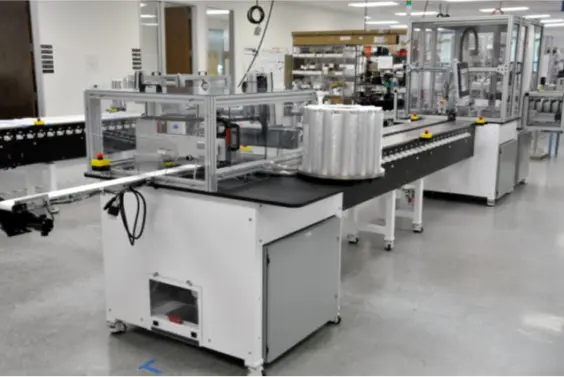
A medical device diagnostic manufacturer needed to rapidly replicate an in-house designed manufacturing tool to support a production ramp-up. The tool included multiple control systems and needed to be…
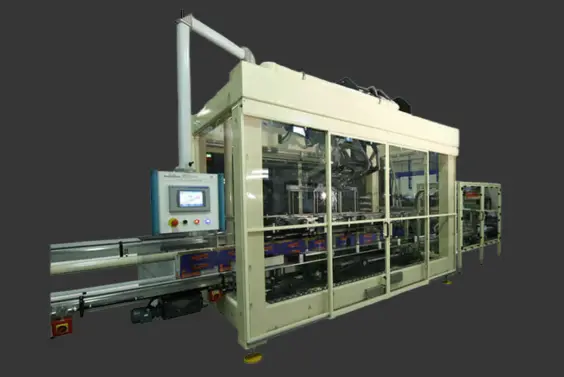
A producer in the bakery industry producing biscuits for retail required a robust automated packaging solution capable of handling demanding, high-volume production requirements. The system needed to deliver…
One of the world’s largest confectionery manufacturers wanted to automate the process of lidding tubs of individually wrapped chocolates. The system needed to pick and place multiple lid types made from…